C91100 Cast Bronze Components for OEM Supply
Rate: US$ 17.90/Kg
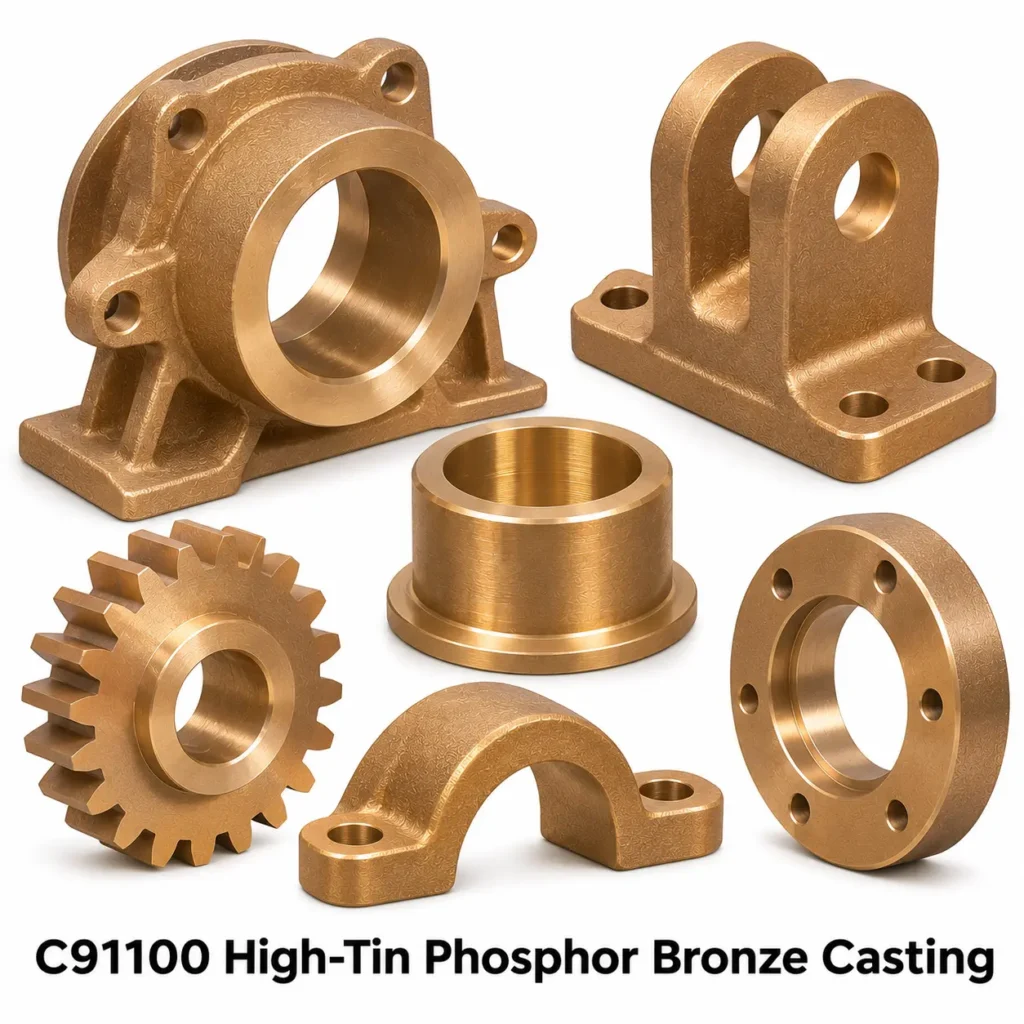
A nominal 16% tin cast bronze used for specialised bearing and load-support components. Often called bridge bronze, it belongs to a distinctly higher-tin family than the common PB1 and PB2 procurement grades. Cable Glands India supplies drawing-based enquiries for C91100 castings and machined parts for specified bridge-bearing elements, pressure plates and engineered sliding parts. Send the controlling material standard, component drawing and annual demand so the casting route and inspection plan can be reviewed before quotation.
Material designation: UNS C91100. Product form: castings and machined cast components. This is a cast tin-bronze page; wrought phosphor-bronze sheet and spring strip grades must not be used as casting equivalents.
Chemical Composition of C91100
The following selected chemical limits are percentages by mass for general alloy identification. The agreed product standard and its current edition govern acceptance, including all residual elements and process-specific provisions.
| Element | Selected limit, wt.% |
|---|---|
| Copper, Cu | 82–85 |
| Tin, Sn | 15–17 |
| Phosphorus, P | 1.0 max, subject to casting-form provision |
| Lead, Pb | 0.25 max |
| Zinc, Zn | 0.25 max |
| Iron, Fe | 0.25 max |
Phosphorus limits may differ for continuous cast material. Do not apply the general table to every product form without checking the ordered specification. These alloys permit residual lead: a low lead limit is not a drinking-water approval, regulatory declaration or guarantee of zero lead.
Equivalent Grades and Specification Cross-Reference
| Designation or family | How to use the comparison |
|---|---|
| UNS C91100 / CDA 911 | Alloy identification; order the exact designation and product standard. |
| British and European comparison | UNS C91100 and CDA 911 identify the same UNS alloy designation. ASTM B22/B22M is an applicable specification route for specified bridge and turntable castings; it is not an alloy equivalent. PB2, C90800 and CuSn12-C / CC483K are not equivalents to this 15–17% tin grade. |
| DIN, JIS and Indian specifications | Submit the full designation and edition for a documented comparison. No blanket DIN, JIS or IS equivalence is claimed. |
Approve substitutions only after comparing chemistry, test-piece requirements, mechanical properties, casting method and application requirements. A similar nominal tin content is insufficient evidence of interchangeability.
Typical Products Made in C91100
- Engineered bridge-bearing plates to approved customer drawings.
- Turntable bearing components to approved customer drawings.
- Specified pressure and thrust plates to approved customer drawings.
- Heavy sliding support elements to approved customer drawings.
- Custom high-tin bronze cast shapes to approved customer drawings.
Supply can be discussed as rough castings, proof-machined blanks or finished machined components. Clearly distinguish the final component dimensions from the dimensions of the casting blank. Bore allowance, parting line, riser removal and datum selection affect both cost and finished-part yield.
Casting Processes and Route Selection
Sand Casting
Sand casting is a flexible route for shaped parts, flanges, plates and components with changing cross-sections. Pattern design, feeding and core placement are reviewed around the final machining envelope. It is particularly useful when the component cannot be produced efficiently from a cylindrical blank.
Centrifugal Casting
Centrifugal casting can be considered for suitable tubes, sleeves, rings and cylindrical blanks. Rotating-mould production requires an appropriate removal allowance on the bore and on other surfaces. The enquiry should state finished OD, ID and length as well as test requirements. Suitability and available sizes are confirmed during quotation.
Shell Mould and Investment Casting Review
For repeat shaped components, shell moulding or investment casting may be reviewed where geometry, quantity and alloy behaviour justify the tooling. These routes are assessed individually; no universal surface finish or casting tolerance is promised for all C91100 components.
Machining from Cast Stock
For some simple components, machining a qualified cast bar or tube can reduce pattern investment. The stock must be certified to the required alloy and product standard. This route is assessed against material utilisation, stock availability, annual demand and inspection access.
Mechanical Properties and Engineering Selection
Strength, elongation and hardness depend on casting method, section size, specimen location and the ordered standard. Request the required minimum values on the purchase drawing rather than treating a generic handbook value as a guaranteed finished-part result. Where mechanical testing is required, agree separately cast versus attached test specimens and the applicable acceptance criteria.
C91100 requires particular attention to ductility, impact, edge loading and casting soundness. Do not substitute it into a PB2 drawing merely to obtain higher hardness. Structural bearing applications require approval by the responsible design engineer.
Bronze bearings still need an engineered lubrication and operating-clearance strategy. Do not describe a plain cast bronze component as self-lubricating unless a separately specified material or lubrication system supports that claim. Corrosion suitability also depends on the actual fluid, temperature, contaminants and flow conditions.
CNC Machining and Finished Casting Features
Drawing-based machining may include turning, boring, facing, milling, drilling, threading, grooves, counterbores and assembly features. Specify the critical fits, surface roughness, concentricity, runout and datum scheme. Tight bore tolerances are quoted after reviewing wall thickness and the stability of the casting.
For bearing components, identify the running surface and oil-groove layout. For rings and gears, identify the locating face and finish-machining sequence. Any mating steel or assembly interface should be included in the technical review when its condition affects performance.
Quality Planning and Inspection Documents
- Chemical-analysis requirements and heat identification agreed with the order.
- Dimensional inspection against the approved drawing and revision.
- Hardness and mechanical tests where specified and agreed.
- Dye-penetrant, radiographic or other inspection where technically applicable and contracted.
- Material certificates, traceability and third-party inspection requirements confirmed in the quotation.
- Packaging and surface protection matched to machined features and transit conditions.
A material certificate does not replace a component inspection report. State which dimensions need recorded results and whether a first-article sample must be approved before production. Inspection scope, sampling and document format form part of the commercial agreement.
Information Required for a B2B Quotation
- 2D drawing and revision, plus a 3D model if available.
- Exact C91100 material specification and casting product form.
- Prototype, batch and annual quantities.
- Finished dimensions, critical tolerances and machining allowance.
- Service load, lubrication and environmental requirements where relevant.
- Required tests, certificates, packing and delivery destination.
Tooling, metal content, casting yield, machining time and inspection scope all affect price. A drawing-based quotation gives a more useful procurement basis than a single universal price per kilogram. Confirm repeat-order forecasts when evaluating tooling economics.
Frequently Asked Questions
Is C91100 a casting alloy or a wrought spring bronze?
It is a cast tin-bronze designation. Wrought strip, sheet and wire alloys use different designations and processing requirements.
Can a similar PB grade be supplied instead?
Only after a documented technical comparison and buyer approval. Nominal composition and common trade names do not establish exact equivalence.
Can parts be supplied fully machined?
Send the finished drawing for a casting-and-machining review. Fits, surface finish, threads and inspection requirements should be included in the enquiry.
Which casting process is best?
Geometry, section thickness, quantity and testing requirements govern the choice. Cylindrical sleeves and shaped plates need different process reviews.
Are material test certificates available?
Specify the required certificate type and testing scope at enquiry stage so document availability and cost can be confirmed before ordering.
Is this alloy automatically approved for drinking water?
No. Chemical composition alone does not establish potable-water compliance. Application-specific certification must be confirmed separately.
Can you quote replacement components?
Supply a dimensioned drawing and the original material requirement. A sample can assist review, but worn dimensions should not be assumed to represent the original design.
What determines the minimum order and lead time?
Component size, tooling, process route, machining and tests determine the practical batch size and delivery plan. These are confirmed with the quotation.
Request a C91100 Casting Quotation
Discuss your C91100 bronze component with Cable Glands India. Send the drawing, quantity, alloy specification and inspection requirements using our contact page. Our team can review the most practical supply route for your application.
Return to Phosphor Bronze Casting and Alloy Selection
Explore All Phosphor Bronze Casting Alloys
Compare our cast bronze alloy pages for composition, grade comparisons, typical products and manufacturing options.