BRASS BOLTS , BRASS COLD FORGED BOLTS
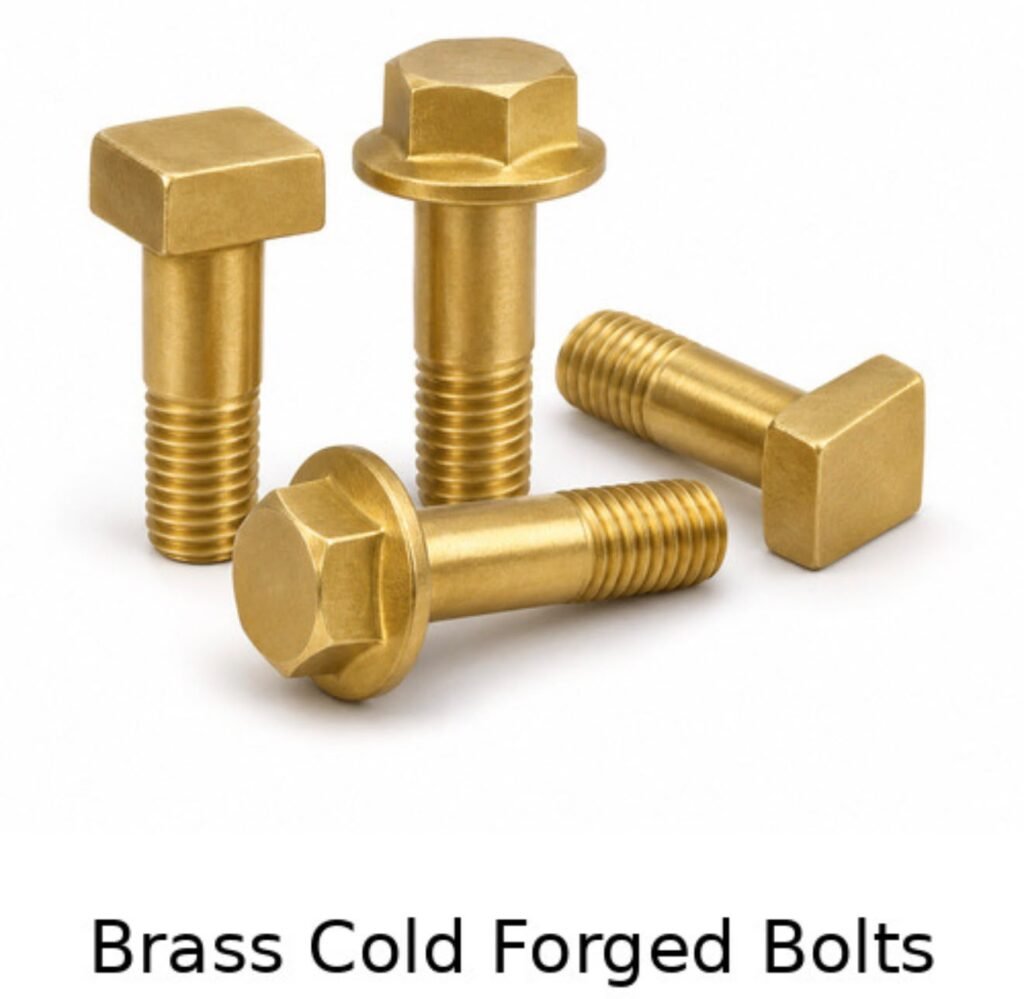
Brass cold forged bolts are headed external-thread fasteners produced from a cold headed brass blank, with subsequent thread formation and any drawing-defined finishing. Cable Glands India reviews bolt requirements for electrical OEMs, EPC contractors, utilities and distributors. Hex, square, round-head square-neck and flange profiles are evaluated against alloy, grip length, bearing geometry and joint performance. The approved application determines whether the bolt is suitable for a given load and environment.
Price: US$ 16/kg
Detailed product overview
Hex-head brass bolts
A hex head provides external wrench engagement. Across flats, across corners and bearing diameter define different aspects of the assembly. Socket wall thickness and surrounding clearance determine access. Keep head height and wrenching height separate where the crown includes a chamfer. Evaluate the fillet at the head-to-shank transition against the washer or mating bore. For a finished bolt, check that the specified tool reaches the intended wrenching flats.
Part-threaded bolts and grip length
An unthreaded grip can locate through a joint stack and keep thread runout away from a critical interface. Specify the length of full usable thread and the maximum runout. Locate the shank diameter and tolerance where the assembly requires a fit. Include washers and spacers in the grip stack. Confirm that the nut seats before it reaches the thread transition.
Fully threaded and tap-bolt designs
A fully threaded design provides adjustment where multiple stack heights are possible. The drawing should identify any required plain land or underhead clearance. Usable thread length can be shorter than overall underhead length because of runout and point chamfer. If the part enters a tapped hole, review the bottoming limit. For a through joint, confirm nut projection with both shortest and longest stacks.
Flange and square-head brass bolts
A flange provides a wider bearing area and may replace a separate washer in a joint designed for it. Define flange diameter, underside profile and runout. A square head can be captured in a dedicated pocket. Check corner radii, nut driver clearance and seating. Large flange-to-shank ratios and sharp corners deserve an individual forming review before tooling.
Round-head square-neck bolts
The neck can seat in a prepared square hole or mating feature to resist rotation. The head and neck must seat before the nut develops the intended clamp. Specify neck length, width, corners and underhead radius. Test rotation resistance on the intended substrate and thickness. Thin or soft mounting plates can distort around the neck if the assembly loads are high.
Shoulder, step and special bolts
A shoulder may define stand-off, alignment or a sliding interface. Set shoulder length against the assembly stack and specify the tolerance over the intended fit diameter. Secondary machining may be evaluated for grooves, cross holes and tight fit features. Head and shank alignment matter when the shoulder guides the assembly. Use the specialty fastener range for parts driven primarily by custom retention or locating features.
Key features
- Hex, square, flange, round-head square-neck and custom step profiles.
- Metric or Unified as specified; full thread, partial thread and grip variants.
- Bearing face, washer, underhead radius, grip and antirotation features as applicable.
- Finished gauges, length and runout, head geometry and agreed joint or load tests.
- Drawing-based material, finish and dimensional review before tooling.
Related engineering terms and design details
Bolt thread and runout
Record the metric or Unified thread designation with fit class and point. Place the maximum runout on the drawing if full engagement is required near a shoulder. Specify the condition at the location where the nut first starts. Check the minimum full-thread length on the finished part. Finish-dependent thread changes should be resolved through final gauging.
Underhead radius and washer clearance
A sharp washer bore can interfere with the formed fillet. Verify washer ID and chamfer at worst-case dimensions and compare them with the bolt section. A washer that sits on the fillet gives an unreliable seating condition. A specified bearing datum makes this relationship easier to inspect.
Torque and joint clamp load
Treat torque as a process setting to be validated on the intended joint. Finish, lubrication and bearing geometry alter the fraction that becomes tension. Test the mating nut, washer and bolt together. Record fixture material, tightening rate and acceptance. If proof load or tensile behavior is required, state the numeric value and method appropriate to the brass fastener.
Electrical equipment joint design
Brass bolts may serve a mechanical or electrical role according to the approved design. The resistance of a joint depends on its contact areas, preload, finish and condition over time. Where contact resistance is important, specify a test on the whole installed assembly. Clarify whether washers or interface compounds are required.
Corrosion and coating interfaces
Consider dissimilar metals, moisture, service temperature and exposure when specifying the assembly. A plating callout should identify material, thickness and significant surfaces. Inspect the thread and wrench fit after finishing. Verify application-specific requirements on the joint, especially where exposed faces are close to insulation or a sealed interface.
Antirotation and installation space
Provide socket clearance and specify whether tightening occurs from the head or nut. Captured square profiles need rotational clearance and support. Test a square neck on a production-intent plate for seating and torque-out. Set a limit for damage or deformation on the receiving feature before first article approval.
Technical specifications
| Characteristic | Specification basis |
|---|---|
| Bolt style | Hex, square, flange, round-head square-neck and custom step profiles. |
| Thread and length | UNC, UNS, UNF, BSW and ISO metric (coarse or fine). Specify pitch or threads per inch, fit, and full-thread or partial-thread length as applicable. |
| Joint interfaces | Bearing face, washer, underhead radius, grip and antirotation features as applicable. |
| Verification | Finished gauges, length and runout, head geometry and agreed joint or load tests. |
| Size range | Nominal thread diameter: 1/8″–2″ (inch range) or 3–50 mm (metric range), depending on design. |
| Dimensional tolerances | Drawing-controlled. Identify finished dimensions and functional datums. |
| Finish | Bare or a drawing-specified coating, subject to application and process review. |
| Ordering units | Price listed in USD per kilogram. Provide delivery quantity by mass or piece count and agree the unit on the quotation. |
Brass grades and international equivalents
| UNS reference | EN or common designation | Alloy family | Procurement note |
|---|---|---|---|
| UNS C26000 | CuZn30 / CW505L | Cartridge brass | Candidate for demanding forming, especially where substantial upset or tail deformation is expected. Verify the feedstock temper and formability with the producing mill. |
| UNS C26800 | CuZn33 / CW506L (comparison) | Yellow brass | Candidate where the selected wire or rod grade and temper fit the geometry. Check both specifications before allowing substitution. |
| UNS C27000 | CuZn36 / CW507L (comparison) | Yellow brass | Compare against the approved chemistry, incoming form and test requirements before any substitution. Qualify fit, finish and forming behavior with samples. |
| UNS C36000 | Free-cutting brass | Machining comparison | Use for route comparison when machining dominates. Evaluate an alternate grade or process if the cold deformation required by the drawing is substantial. |
| UNS C69300 | CuZn21Si3P / CW724R | Silicon brass | Lead-free specification candidate subject to approved chemistry and application requirements. Evaluate the actual forming route and feedstock before committing to a cold forged design. |
Use these designations as cross-reference guidance. National standards may specify different compositional limits, allowable product forms, delivery conditions and mechanical properties. The approved material specification and lot documentation govern acceptance. Review the alloy and temper for the cold work required by the drawing.
Product types and variants
| Family | Typical scope | Design review |
|---|---|---|
| Hex-head brass bolts | A hex head provides external wrench engagement. | Check drawing, fit surfaces and the relevant assembly test before first article approval. |
| Part-threaded bolts and grip length | An unthreaded grip can locate through a joint stack and keep thread runout away from a critical interface. | Check drawing, fit surfaces and the relevant assembly test before first article approval. |
| Fully threaded and tap-bolt designs | A fully threaded design provides adjustment where multiple stack heights are possible. | Check drawing, fit surfaces and the relevant assembly test before first article approval. |
| Flange and square-head brass bolts | A flange provides a wider bearing area and may replace a separate washer in a joint designed for it. | Check drawing, fit surfaces and the relevant assembly test before first article approval. |
| Round-head square-neck bolts | The neck can seat in a prepared square hole or mating feature to resist rotation. | Check drawing, fit surfaces and the relevant assembly test before first article approval. |
| Shoulder, step and special bolts | A shoulder may define stand-off, alignment or a sliding interface. | Check drawing, fit surfaces and the relevant assembly test before first article approval. |
Industrial applications
| Application | Typical procurement requirement |
|---|---|
| Power distribution enclosures | Equipment hardware, panel supports and approved terminal assemblies. |
| EPC projects | Drawing-controlled hardware for assembly packages with defined fastener schedule and finish. |
| Utility and distributor supply | Specified brass replacements with verified thread and installed envelope. |
Manufacturing process
How to specify the part on a drawing
Start with an installed assembly view and a separate detail of the loose fastener. The assembly view identifies mating components, access for tools, neighboring parts and the required service position. The detail establishes dimensions that can be measured on incoming material. Use a section view when an internal surface, depth or transition controls fit. Give each critical dimension a datum and state whether the limit applies before or after finishing. The same dimension should have a single controlling callout. A purchase order should identify the released drawing revision and any governing specification so two suppliers can interpret the part consistently.
Feasibility of the cold forming route
The sequence starts by deciding how much metal needs to move at each die station. The finished shape is considered together with the feedstock diameter, material condition, lubricant, tool access and method of ejecting the blank. A large change in section may need multiple forming operations. Metal must be able to flow into the head or flange without producing folds at the transition. Sharp corners, narrow webs and asymmetric masses can require radius changes or a secondary operation. Where a radius is part of the application, the drawing should show which mating geometry provides clearance so it can be reviewed before tools are made.
Incoming material and lot identity
Define the alloy by designation and a material specification suitable for the incoming wire or rod. Temper, dimensions and surface condition can be as important to heading as chemical composition. Receive material with the lot identity and documentation agreed in the order. Where chemistry verification is required, specify the method and limits on the inspection plan. Verify lead and other restricted substances against the applicable customer requirement and the actual grade. Keep the incoming lot connected to the production and finishing batches so a process change or returned part can be traced. An equivalence table helps with purchasing discussions but the approved drawing and certificate govern acceptance.
Cutoff, blank development and forming
A cutoff establishes the volume available to fill the finished geometry. Consistent cutoff mass, straight feed and a sound end condition support repeatable formation. The first station can prepare a blank for a controlled upset. Later stations develop the profile, size an important diameter or create an internal recess where applicable. The tooling sequence and checks depend on the product. Trial blanks should be inspected at intermediate operations so a defect can be traced to the stage that created it. Record the approved first pieces before production and recheck the relevant characteristics after tool adjustment or replacement.
Secondary operations and cleaning
Secondary machining can establish a dimension that requires a tighter tolerance, a controlled finish or a feature that is difficult to form with an axial tool. Call out whether each functional feature may be machined or must remain as formed. Burrs at holes, grooves and transitions can interfere with plating or assembly. State the allowed edge condition rather than assuming a general deburr note gives the desired result. Use a cleaning process compatible with the finish and the end application. Check hidden recesses when they can retain lubricant, chips or debris. A finished part should be measured after the operations that can affect its fit.
Coating specification and inspection
A finish callout should identify the coating, significant surfaces, required thickness, any undercoat and the method used to verify it. The agreed acceptance condition should also address color or cosmetic appearance when the part remains visible. Internal features, recessed faces and narrow pockets can be difficult to measure. Select reference surfaces or an appropriate test section before the order is released. Specify the dimensions that must be checked after finishing and the relevant gauge condition. Use finished parts for assembly tests because friction, clearance and electrical behavior can differ from the bare part. If a coating requires masking, show the boundary on the drawing.
Quality standards, certifications and inspection
| Requirement | What to specify |
|---|---|
| Quality management | ISO 9001:2015 quality management system. Where a certificate is required, request its current edition, applicable scope and manufacturing site. |
| Dimensional references | ISO 4014, ISO 4017, ASME B18.2.1 and ASME B18.5 offer dimensional references for applicable headed forms. Declare the specific reference and edition and confirm deviations on the approved detail. Select the actual alloy, strength and installation criteria for the brass joint. A flange bolt with an integral bearing surface can change joint height and tool access, so compare the entire stack rather than matching overall length alone. For a square-neck head, test the plate geometry and retention under the intended installation torque. State how the head, washer and receiving hole are oriented in the test. |
| Thread specification | Specify ISO metric or Unified thread form and fit where applicable, using the agreed thread standard and gauge condition. |
| Material report | Request traceable alloy and temper documentation. Specify the incoming product form and the required report format at enquiry. |
| Regulatory declarations | Provide the applicable RoHS or REACH documentation requirements and any restricted-substance criteria. The declaration depends on the part, grade and application. |
| Approval records | Agree first article measurements, functional test reports, control plan or PPAP submission requirements before production. |
First article approval
Set the first article scope before tooling starts. A report can map measured values to numbered drawing callouts and identify the actual alloy, finish and sample lot. Use an inspection fixture that matches the drawing datums. Separate variable measurements, such as a measured height, from attribute checks, such as acceptance by a functional gauge. Confirm who approves the first article and which changes trigger resubmission. Where the result depends on a mating part, supply representative hardware or a controlled test fixture. Samples used for functional approval should identify their process route so prototype results are interpreted in context.
Production control and sampling
A control plan can identify where each characteristic is checked, how it is measured and what action follows a failed sample. High-risk characteristics may call for different checks from general dimensional features. If the purchase requires a particular sampling procedure, specify the inspection level and acceptance criteria alongside the test frequency. For automatic sorting, define the detectable defects and set up representative limit samples where appropriate. After a stoppage or tool change, identify the first-off verification needed before continuing. Keep the inspection lot linked to the accepted shipment and isolate suspect material while measurements are reviewed.
Measurement and calibration
Choose a measurement method that can resolve the drawing tolerance and reach the actual feature. Use an optical system, fixture, thread gauge or dimensional instrument according to the inspection plan. A measurement at the edge of a radius can vary with fixturing even when the part is stable, so define the measurement location. If the buyer will perform a different incoming method, compare results on the same samples before routine supply. Identify gauge size, tolerance class and condition where relevant. For disputed results, retain samples with lot records and use an agreed reference method.
Assembly validation and use limits
An assembly can fail through the receiving component, coating, fit or installation method even when every loose fastener dimension passes. Use the production-intent mating materials and the intended tools for validation. Define maximum and minimum assembly conditions where variation affects the outcome. Record the loading direction, tightening or setting sequence, and how failure is judged. For electrical equipment, distinguish a dimensional check from qualification of the equipment or verification of continuity through a finished joint. Where vibration, heat, moisture or chemicals affect performance, identify the applicable tests and acceptance criteria with the equipment designer.
Packing and incoming inspection
The packaging method should protect formed heads, edges and coating and should preserve the identity of each lot. Identify part number, revision, quantity, finish and lot information on the package where required. A buyer feeding components automatically may need an agreed cleanliness level or packing arrangement. Small mixed variations can look alike, so separate revisions, sizes and finishes in order lines and containers. Retain enough samples to compare a delivered lot with its approval data if a fit issue arises. Define the receiving inspection that will be used for subsequent deliveries and record any deviations through a controlled approval.
Engineering changes and repeat supply
When a drawing or finish changes, review the effect on dies, gauges, fixtures, sample approval and inventory. Changes in mating hardware can also affect fit even when the fastener drawing stays the same. Identify which revision a given order must receive and whether the new part is interchangeable with current stock. Avoid mixing revisions in the same container unless the customer has agreed to it. On repeat orders send the released documents and reference the approved sample or inspection plan. Flag any change in annual demand, application, packaging or test method when requesting updated pricing.
Why choose Cable Glands India
Cable Glands India reviews drawing-defined fasteners in Jamnagar, Gujarat, India. Request production samples and an agreed inspection plan. Enquiries are welcome from India, the United States, the United Kingdom and other export markets.
Establish the purchase baseline
Include a part number, drawing revision, exact alloy and finish code, annual requirement and anticipated release quantity in the RFQ. Flag a mandatory manufacturing route, such as an as-formed bearing seat, when it is a design requirement. State the units for dimensions and distinguish shop tolerances from functional limits. If the part replaces hardware in an installed assembly, attach the approved earlier drawing or confirm which interfaces must match it. A quantity estimate is useful for tooling review, and lot size helps determine a sensible inspection and delivery plan. Keep samples identified by revision when multiple alternatives are submitted.
Separate dimensional and functional approval
Use dimensional inspection to confirm the component detail. Use an approved assembly fixture or representative mating parts to verify the performance expected in service. Put the numeric criterion, test method and acceptance condition on the purchase documents. Test reports should identify whether samples are bare or finished and whether fixtures reproduce the receiving part. If production tooling is required to reproduce a feature or material condition, qualify parts from the actual tool sequence. Confirm whether any tested or sectioned specimens are retained for records or excluded from the delivery quantity.
Confirm supply scope with the quote
The listed rate gives purchasing teams a common reference in USD per kilogram. A formal quotation identifies the drawing, alloy, finish, inspection scope, volume and any tooling or sample charges. State the destination and packing requirement to align the quote with the delivery program. If parts are supplied in piece counts, agree on the pricing and shipment units to avoid conversion differences. Identify any documentation that must travel with each lot. Cable Glands India can review the part and related fasteners as one enquiry while keeping each drawing revision and acceptance requirement separate.
Frequently asked questions
How are bolts and screws separated here?
The bolt range focuses on headed joint fasteners with specified grip, mating nut and load transfer. The screw page covers driven machine and terminal styles.
How do I define grip length?
State the required unthreaded shank from the head datum, then relate it to all plates, washers and spacers.
Can the bolt be threaded up to the head?
Show the allowable runout and the first location that needs a complete thread. The head and tooling envelope influence feasibility.
Do standard steel torque tables apply?
Use the assembly-approved brass bolt and nut data. Material, finish and load requirements must be verified for the actual joint.
Can you supply a square-neck form?
Submit the head, neck and shank dimensions with the matching pocket or plate specification for review.
Which head dimensions belong on the drawing?
Include across flats, head height, bearing diameter and underhead radius where these are functional.
How should plated bolts be gauged?
Agree the final thread and wrenching checks on finished samples and identify the required thread class.
What do you need to quote a custom shoulder bolt?
Send shoulder diameter and length, datum, fit tolerance, thread runout and the mating part interface.
What is the listed price?
US$ 16/kg is the listed rate. Submit the drawing, finish and quantities for a formal quotation.
Equivalent product and related terms
| Language | Trade terms |
|---|---|
| Spanish | Pernos de latón forjados en frío, pernos hexagonales, pernos con brida |
| Russian | Латунные болты холодной высадки, болты с шестигранной головкой, фланцевые болты |
| French | Boulons en laiton forgés à froid, boulons à tête hexagonale, boulons à embase |
| Portuguese | Parafusos de latão forjados a frio, parafusos sextavados, parafusos flangeados |
| Italian | Bulloni in ottone stampati a freddo, bulloni a testa esagonale, bulloni flangiati |
Related brass fasteners and parts
- Brass Cold Forged Parts and Cold Forged Components
- Brass Cold Forged Nuts
- Brass Cold Forged Screws
- Brass Cold Forged Rivets
- Special Brass Cold Forged Fasteners
- Brass Bolts
Request a quotation
Send your drawing, alloy, finish, order volume and delivery destination. Include mating parts, inspection requirements and approval schedule.