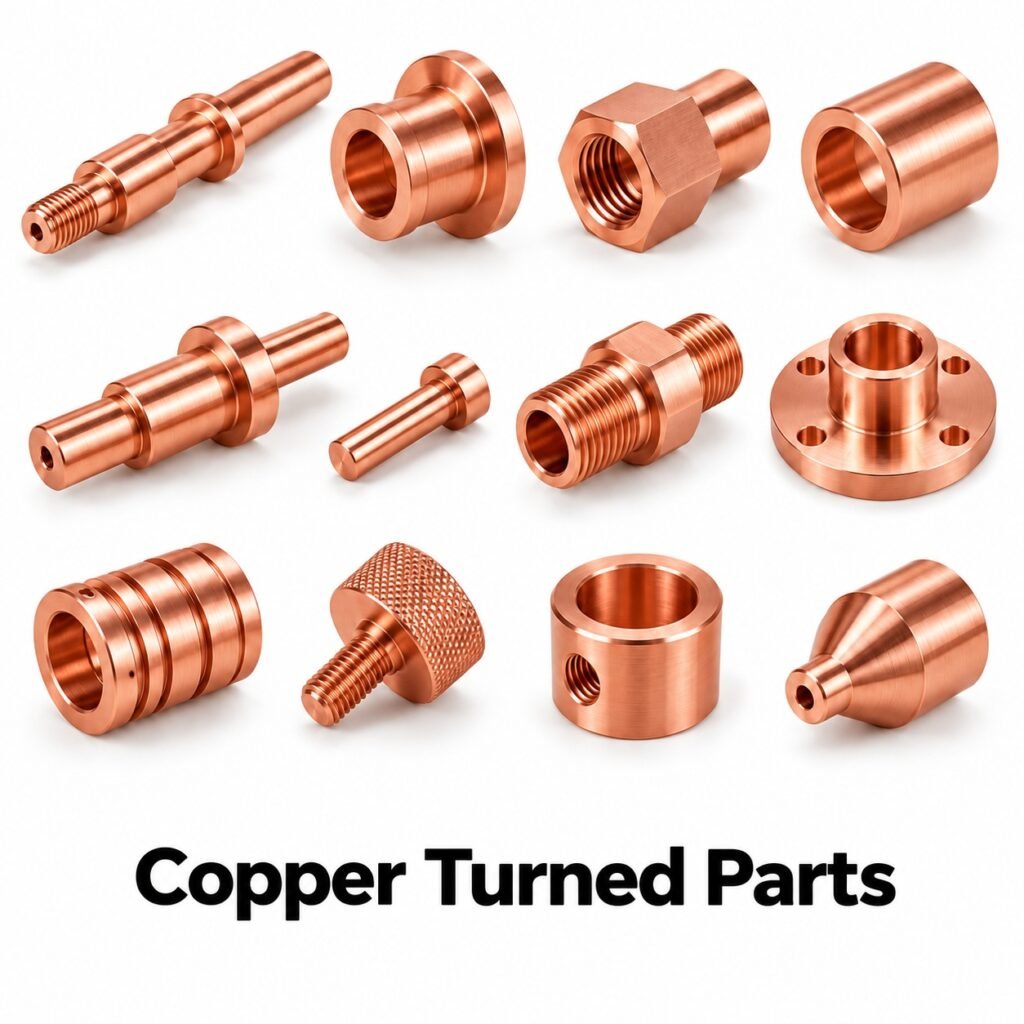
Copper Turned parts
Price: US$ 19/kg
Cable Glands India manufactures copper turned parts for electrical OEMs, EPC contractors, power utilities and industrial distributors. These drawing-based copper components are produced by precision copper turning and secondary machining, with material grade, threads, functional dimensions and surface finish defined for the intended assembly. The product family includes transformer studs, contact pins, terminal bodies, conductive sleeves, threaded connectors, electrical bushes, heat-transfer parts and custom copper fittings. Supply requirements are reviewed against customer drawings, samples and the agreed inspection plan.
Detailed Product Overview
Copper Turned Electrical Studs and Terminals
Copper studs and terminals provide conductive interfaces in transformers, switchgear and power distribution equipment. The main engineering requirements include conductor contact area, thread engagement, shoulder geometry and the path taken by the current. A component’s ampacity cannot be assigned from its material name or mass alone. Joint pressure, connection torque, plating, temperature rise and the mating conductor all contribute to performance. The drawing should identify electrical contact faces separately from clearance surfaces and state whether functional connection testing is required as part of the supply scope.
Precision Copper Contact Pins and Connector Bodies
Contact pins and connector bodies can combine a locating diameter, lead-in chamfer, threaded region and connection surface. Small changes in contact geometry may alter insertion force or the real area of electrical contact. Machining therefore needs a clear definition of functional diameters and the surfaces that must remain free of damage. A copper connector intended for a spring contact differs from a bolted terminal. The mating system, contact finish and assembly requirements should be reviewed together, with dimensional inspection complemented by functional testing where the customer specification requires it.
ETP Copper Turned Parts for Conductive Assemblies
Electrolytic tough-pitch copper is used for many electrical and thermal components. The selected product condition affects strength, ductility and machining behavior, so a generic request for pure copper is insufficient for a controlled supply. Thin walls and fine threads require particular attention to burr formation and handling damage. Drawings should specify the actual material designation and any conductivity requirement, including the test basis. Where the part will be exposed to a joining or heating process, the designer should assess whether the chosen copper grade suits that process environment.
Oxygen-Free Copper Machined Components
Oxygen-free copper may be specified where oxygen content or the behavior of the material during subsequent processing is important. The exact grade should be stated because oxygen-free copper and oxygen-free electronic copper are separate procurement designations. A customer reference to OFC needs clarification before substitution. Material certification should identify the supplied grade and condition, with any additional analytical or electrical testing agreed during quotation. Machined components should also be protected against surface contamination, since cleaning and joining requirements can be sensitive to residues that remain after turning or packaging.
Tellurium Copper Turned and Threaded Parts
Tellurium-bearing copper is a material option when machinability and conductive performance must be balanced in a detailed turned component. Examples include threaded connectors, contact carriers and small terminal elements. It should not be treated as chemically identical to unalloyed ETP copper. The drawing should identify the selected UNS or EN grade and the properties that matter to the application. When a customer proposes switching to a more machinable copper, the engineering review should address electrical, thermal, joining and service requirements before the alternative becomes an approved production material.
Copper Sleeves, Bushes and Thermal Interfaces
Copper sleeves and bushes can serve as conductive links, thermal paths or locating features within a larger assembly. Their function determines the required fit, surface roughness and dimensional controls. A heat-transfer interface may depend on contact pressure and flatness as much as on bulk material conductivity. Thin copper sections can distort under clamping or be damaged during installation. The machining and inspection plan should therefore consider wall support, free-state dimensions and the assembly sequence. Thermal or electrical ratings should be established at assembly level when they are part of the specified performance.
Copper Threads, Plating and Contact Surface Protection
External and internal copper threads need attention to material softness, burr control and assembly load. Fine threads should be assessed against engagement length and the potential for damage during handling. Tin or another specified coating may be used for a particular connection design, but coating thickness and final thread acceptance must be coordinated. Contact surfaces should be protected from scratches, contamination and packing damage. A visual color change does not by itself define electrical suitability, so acceptance criteria should distinguish normal surface condition from defects that affect the intended joint or finish.
Key Features of Copper Turned parts
- Drawing-based copper manufacturing with defined material and revision control.
- Turned diameters, bores, shoulders, grooves and specified threads.
- Secondary drilling, tapping, slotting and milling where required.
- Surface finish and edge condition specified for functional interfaces.
- Material and production-lot traceability to the agreed order scope.
- Inspection documentation and protected packing defined for the application.
Datum-Controlled Precision and Repeatability
The useful precision of a machined part is the precision of its functional interfaces. Diameters, shoulders, bores and mounting faces should be related to a coherent datum system so that inspection represents the assembled condition. Very tight limits on nonfunctional surfaces can add cost without improving performance. For copper components, we review how the workpiece is held, which surfaces are machined together and how critical dimensions are measured. Approved first-off results establish a production reference. Subsequent checks should address tool wear, setup changes and the features most likely to influence the customer’s fit or function.
Threaded Connections and Gauge Acceptance
Threads are defined by form, diameter, pitch, tolerance class and usable engagement, rather than by a nominal size alone. Drawings may require metric, unified, BSP parallel, BSP taper or NPT connections, each with its own inspection basis. A threaded hole also needs adequate drill depth, clearance and a defined entry chamfer. For copper threaded components, gauge acceptance should be coordinated with the specified surface treatment. Where coating changes the effective thread dimensions, the order should state whether gauges apply before finishing, after finishing or at both stages, with the relevant acceptance class recorded.
Controlled Surface Finish and Edge Condition
Surface roughness should be assigned to the particular sealing, sliding, contact or locating surfaces that need it. A general statement such as polished finish does not define a measurable requirement. We distinguish machining texture, cosmetic appearance, burr removal and edge rounding during drawing review. The component may need a controlled chamfer at an assembly entry while another edge must remain sharp for a defined function. On copper parts with intersecting holes, inspection should consider internal burrs as well as accessible edges. Cleaning and handling requirements should preserve the accepted surface until installation.
Custom Geometry and Secondary Operations
A turned blank can receive cross drilling, slotting, flats, pockets, tapped holes and other milled details. Planning these operations together helps maintain the relationship between the principal axis and the secondary geometry. Tool access, fixturing and inspection access should all be considered before the design is frozen. A blind pocket needs a practical cutter radius and a defined bottom condition. A radial hole may need angular orientation relative to wrenching flats. The agreed manufacturing route for copper components should also identify which operations occur before finishing and which require final inspection after the last material-removal step.
Material Identity and Batch Traceability
The material designation should remain connected to the production lot through receipt, machining, finishing and dispatch. A trade name or a visual color check is not a substitute for an agreed grade specification. Where certification is required, the purchase order should identify the document type and the information needed to connect the certificate to the supplied parts. For copper orders involving several similar variants, segregation and labeling are especially useful. Proposed substitutions require customer approval. Traceability depth, retention periods and any part marking should be defined according to the customer’s application rather than assumed to be identical for every order.
Finishing, Cleaning and Protected Packing
The finish schedule should identify coating material, thickness, coverage, appearance and any functional areas that require masking. It should also state whether dimensions are controlled before or after treatment. Cleaning requirements depend on the application: an ordinary mounting spacer and a part with an internal fluid passage may need different acceptance criteria. Copper components should be packed to avoid dents, thread damage, surface contamination and mixing of variants. Protective caps, separators or individual wrapping can be specified where appropriate. Packaging is planned around the component’s functional surfaces and the customer’s receiving process, rather than appearance alone.
Technical Specifications
| Parameter | Supply and engineering basis |
|---|---|
| Product family | Copper Turned parts |
| Material | copper; exact grade and condition to drawing |
| Manufacturing route | precision copper turning and secondary machining |
| Dimensions | Custom dimensions to approved drawing; feasibility reviewed before order |
| Tolerances | Feature-specific drawing tolerances and geometric requirements |
| Threads | Metric, UNC, UNF, BSPP, BSPT or NPT as specified; class and gauge basis agreed |
| Surface roughness | Specified for each functional surface; Ra requirement to drawing |
| Finish | Natural machined or specified compatible treatment; coating thickness agreed |
| Inspection | Dimensional, visual, material and functional checks to agreed scope |
| Documentation | Drawing revision, batch identification and ordered inspection records |
| Packing | Protection for threads, contact faces and precision surfaces |
| Price | US$ 19/kg |
Size, strength, pressure rating, current capacity and temperature limits are not universal properties of a custom machined product family. They depend on the material condition, component design, mating assembly and test requirements. State those requirements in the enquiry so that the quotation and inspection plan address the intended service.
Raw Material Grades
Copper grades differ in oxygen content, alloy additions, conductivity and machinability. High-conductivity ETP copper, oxygen-free copper and tellurium-bearing copper should be selected against the electrical, thermal, joining and machining requirements of the actual component.
| Grade or designation | Material family | Typical selection context | Procurement note |
|---|---|---|---|
| C11000 | UNS ETP copper | Electrical studs, terminals and turned conductive parts | Temper and conductivity specified |
| C10200 | UNS oxygen-free copper | Specified oxygen-free conductive components | Confirm oxygen and product requirements |
| C10100 | UNS oxygen-free electronic copper | Applications requiring the designated purity class | Not interchangeable with all OF copper |
| C14500 | UNS tellurium-bearing copper | Detailed machined connectors and threads | Confirm electrical and joining requirements |
| CW004A / Cu-ETP | EN ETP copper; nearest old BS C101 | Electrical and thermal components | BS C101 is not UNS C10100 |
| CW118C / CuTeP | EN tellurium copper; legacy BS C109 reference | Machined copper components | Compare specification before substitution |
International Material Equivalents and Cross-References
The following table is an engineering cross-reference, not a declaration that every designation is interchangeable. Check chemical limits, product form, condition, mechanical requirements and the governing specification before approving an alternative. Legacy BS numbers and UNS numbers may look similar while describing different materials.
| Material family | UNS reference | EN / legacy BS reference | Equivalence limitation |
|---|---|---|---|
| ETP copper | C11000 (UNS) | CW004A / Cu-ETP; BS C101 | Common family comparison; verify limits |
| Oxygen-free copper | C10200 (UNS) | CW008A / Cu-OF; BS C103 | Confirm exact product specification |
| Oxygen-free electronic copper | C10100 (UNS) | CW009A / Cu-OFE; BS C110 | Different numbering systems; verify purity |
| Tellurium copper | C14500 (UNS) | CW118C / CuTeP; BS C109 | Comparable material family; approval required |
Product Types and Variants
| Variant | Important drawing requirements |
|---|---|
| Plain turned components | Outside diameter, bore, length, chamfers and locating shoulders |
| Internally threaded parts | Thread class, full thread depth, drill clearance and entry condition |
| Externally threaded parts | Thread form, engagement length, runout and final finish |
| Shouldered and stepped parts | Datum sequence, concentricity or runout, and shoulder positions |
| Cross-drilled or slotted parts | Hole position, orientation, passage intersections and burr control |
| Turned and milled combinations | Flats, pockets, mounting holes and relationship to the turned axis |
| Finished and marked variants | Coating, masking, part identification and acceptance after treatment |
Related sizes can be organized as a controlled part family, but each variant needs its own identifier and dimensional schedule. A change in thread, material grade or coating can change the functional behavior even when the overall shape appears identical. Sample approval should identify the particular variant and revision assessed. This prevents one accepted sample from being incorrectly used as authorization for several unreviewed versions.
Applications in Electrical and Industrial Equipment
| Customer or industry | Component role | Engineering information to provide |
|---|---|---|
| Electrical OEMs | Connection, mounting, spacing and equipment interfaces | Contact geometry, assembly torque, insulation clearances and test scope |
| Transformer and switchgear manufacturers | Terminals, fittings, bushes and conductive or structural interfaces | Mating drawing, material, thread and operating requirements |
| EPC contractors | Project-specific components and installation hardware | Project specification, approved drawing and documentation schedule |
| Power utilities | Replacement or specified equipment components | Equipment identity, service conditions and qualification requirements |
| Industrial equipment builders | Turned and milled parts for mechanical and process assemblies | Loads, fits, environment and finishing requirements |
| Distributors | Controlled stock variants and repeat component supply | Part-number schedule, packing, labeling and revision requirements |
Application examples identify possible component roles; they do not assign an equipment rating or approval. A connector body, spacer or threaded adapter must be assessed within its final assembly. The designer should confirm the relevant electrical, mechanical, environmental or pressure requirements. Where the part is a replacement, compare the complete specification rather than only the visible dimensions, especially if the original material or finish is unknown.
Manufacturing Process
The production route for copper turned parts is planned around the drawing’s functional features. Turning and secondary operations are sequenced to preserve datum relationships, limit handling damage and maintain inspection access. The stages below describe the manufacturing review; the approved order defines any additional tests, sample submissions or special processing.
| Stage | Manufacturing control |
|---|---|
| Drawing review | Confirm revision, material, dimensions, datums, thread forms, finishing and inspection requirements. Resolve missing information before manufacturing. |
| Material preparation | Select approved stock or blank; verify grade, product condition and required material documentation. |
| Setup and first-off | Plan workholding and tool access. Check the first finished part before releasing the production run. |
| Machining | Produce the specified turned and secondary features, monitoring critical dimensions and tool wear throughout production. |
| Deburring and finishing | Control edges and internal intersections. Clean and apply specified treatments, allowing for final dimensional acceptance. |
| Final inspection and dispatch | Verify the agreed characteristics, segregate nonconforming parts and release identified lots with ordered documentation and protective packing. |
Quality Standards, Inspection and Certification Scope
Dimensional Inspection and Measurement Planning
The inspection plan should identify the characteristic, instrument, frequency and acceptance limit. A caliper may be suitable for a general clearance dimension while a close-fit bore requires a different measurement method. Runout, position and flatness are geometric requirements and should be checked against the stated datums. Thread plug or ring gauges assess the specified thread condition; they do not establish every other feature of the component. Where measurement uncertainty is significant relative to the tolerance, the method and the acceptance decision need discussion before the production lot is released.
Material Standards and Compliance Documentation
Material standards define grades and product forms; they do not automatically certify the complete finished assembly. A bar-stock certificate should be reviewed against the purchased grade, condition and relevant test requirements. RoHS, REACH, lead restrictions or application-specific declarations must be addressed for the actual material and finish supplied. Some machinable alloys contain intentional additions, so a generic claim that all metal parts are lead-free would be inappropriate. The requested declaration, applicable requirement and supporting evidence should be identified during quotation and carried into the order documentation.
Quality Systems, Certificates and Customer Approvals
Quality-system certification and product approval are different subjects. An ISO 9001 certificate, where applicable to the supplying operation, should be reviewed for its current validity and scope. A product may separately require a customer qualification, a dimensional submission or testing within an approved assembly. UL, IEC, NEMA, ATEX, NAMAS or another designation should not be applied to every custom machined part as a blanket approval. When a project needs a particular certificate or approval, request the exact document and confirm that the part, manufacturing site and ordered scope are covered.
| Requirement | How to define it on an order |
|---|---|
| Drawing and geometric tolerancing | State the applicable drawing conventions, datum scheme and revision |
| Thread standards | Identify ISO metric, ASME unified, ISO 228, ISO 7 or ASME B1.20.1 requirements as applicable |
| Material product specification | Specify the exact alloy and relevant rod, bar, forging or stock standard |
| Inspection certificate | Request the required material document type; EN 10204 3.1 only when specified and supported |
| Restricted substances | Identify applicable RoHS/REACH and lead requirements for the actual grade and finish |
| Quality-system certificate | Request current certificate and scope for the supplying operation |
| Assembly or project approval | Identify the required test, authority, approved design and acceptance evidence |
Why Choose Cable Glands India
Choose a manufacturing partner on the basis of its response to your drawing, material requirements and inspection needs. Cable Glands India offers a single point of enquiry for copper turned parts and related metal components. The technical discussion focuses on manufacturability, functional interfaces, specification clarity and repeat-order control. This is especially useful where a purchased component combines a standard connection with a custom body or a customer-specific mounting arrangement.
For OEM purchasing, a complete quotation review makes material, finishing, inspection and packing requirements visible before production. EPC contractors can include project documentation and approval requirements in the same review. Distributors can define a family of controlled variants with consistent identifiers and receiving labels. Buyers serving India, the USA, the UK, European markets, Canada and Australia should state their destination-specific requirements and delivery terms so that the offered supply matches the order rather than an assumed market standard.
Frequently Asked Questions
What are copper turned parts?
Copper Turned parts are drawing-based copper components manufactured by precision copper turning and secondary machining. The range includes transformer studs, contact pins, terminal bodies, conductive sleeves, threaded connectors, electrical bushes, heat-transfer parts and custom copper fittings. Each part is specified by its material, geometry, finish and acceptance requirements rather than by a general trade description alone.
What is the price of copper turned parts?
The listed rate is US$ 19/kg. Send the drawing, material grade, quantities and finishing requirements so that the quotation can identify the ordered manufacturing scope, inspection documents, packing and delivery terms without leaving essential requirements undefined.
Which material grades can be specified?
C11000, C10200, C10100, C14500 are included in the grade selection discussion. The actual order must name the chosen material and product condition. Alternative grades require engineering review and approval; a cross-reference table alone does not authorize substitution.
Can you manufacture from customer drawings or samples?
Yes. Custom parts are reviewed against the supplied drawing revision. A sample can support geometry and fit assessment, but missing tolerances, material details and functional requirements need agreement. If a drawing is developed from a sample, it should be approved before production release.
What dimensions and tolerances are available?
Dimensions and tolerances are reviewed for the individual component, selected material, workholding and inspection access. State the critical diameters, datum relationships, fit requirements and surface roughness on the drawing. No universal tolerance or dimensional range is implied for every part in this family.
Can metric, unified and pipe threads be supplied?
Metric, UNC, UNF, BSPP, BSPT and NPT threads can be reviewed against the drawing. Specify the exact form, nominal size, pitch, tolerance class and engagement length. Pipe threads and ordinary fastening threads have different functions and should not be substituted by nominal diameter alone.
Are plating and other surface treatments available?
The required natural finish, coating or surface treatment is reviewed for material compatibility and application. Specify coating type, thickness, coverage and final acceptance condition. Thread and fit inspection must account for the treatment, especially where a coating changes effective dimensions or contact behavior.
Which inspection reports and certificates can accompany an order?
The order can define dimensional reports, material certificates, finishing records and other agreed inspection documents. Request the exact document type during quotation. Project-specific functional tests, third-party inspection and approval submissions require a defined scope rather than being assumed for all custom components.
Do these parts automatically carry electrical or pressure approvals?
No. A machined component is supplied to an agreed specification. Electrical, pressure, ingress-protection or hazardous-area performance depends on the design, tested assembly and applicable approval scope. Any required component approval or assembly test must be identified and verified for the actual application.
What information is needed for a quotation and repeat supply?
Provide the drawing and revision, material designation, quantity, annual demand, surface finish, inspection scope and delivery destination. Include critical application details and any mating gauges or samples. Repeat orders should identify the approved revision and any changes in material, coating, marking or packing.
Equivalent Search Terms in Other Languages
These technical phrases help international buyers identify the product family. They are search-term equivalents; the controlled drawing and agreed material specification remain the basis of manufacture.
| Language | Related terms |
|---|---|
| Spanish | piezas torneadas de cobre; componentes mecanizados de cobre; torneado de cobre |
| Russian | точеные детали из меди; токарная обработка меди; медные контактные детали |
| French | pièces tournées en cuivre; composants usinés en cuivre; décolletage cuivre |
| Portuguese | peças de cobre torneadas; componentes usinados de cobre; torneamento de cobre |
| Italian | parti tornite in rame; componenti lavorati in rame; tornitura rame |
Linked Parts and Related CNC Product Terms
Explore the CNC Machined and Milled Parts category and the related product families below. Each family has its own material selection, manufacturing notes and enquiry requirements.
- Brass CNC Machined Parts
- Brass Screw machine parts
- Stainless Steel CNC turned parts
- Copper Turned parts — current product family
Request a Quotation for Copper Turned parts
Listed rate: US$ 19/kg. Send the latest drawing revision, selected material grade, quantities, annual demand, thread details, functional tolerances, required finish and inspection documents. Include the destination, packing instructions and any sample or project-approval stage. If the component must match a mating part, provide that interface drawing or an approved reference sample so the relevant fit can be reviewed.
Contact Cable Glands India for a technical review and quotation. State any proposed material alternative or drawing change before ordering, so the reviewed specification and the production requirement remain aligned.